
Jinren JR-4200 Long-Profile Trial Checklist
Verify stock support, tool reach and feature spacing on the longest profile in your order mix.
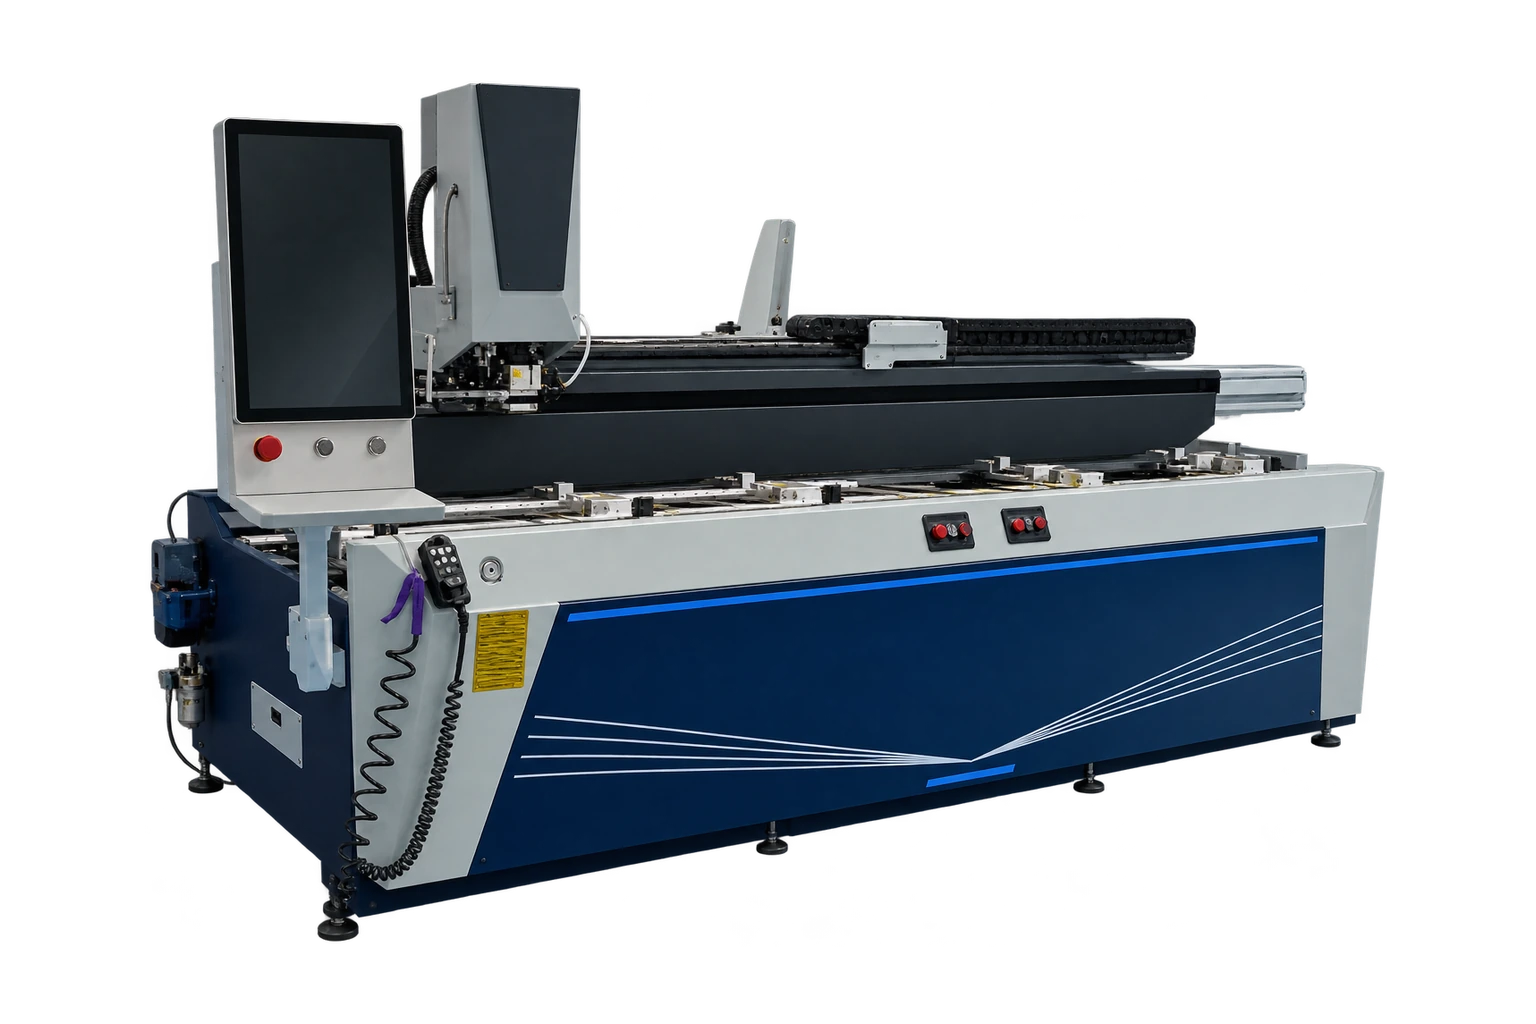
Build the trial around the outermost features
The JR-4200 catalogue lists 4,200 mm of X-axis travel. Mark the finished stock length and the distance between the first and last feature as separate values. Give the supplier the tool approach at each end and identify any material that extends beyond the feature span.
Watch how the extrusion is supported
Have the installer confirm the support arrangement for the actual length and section. Check seating at the reference stop and inspect whether the part moves as it is clamped. Confirm clearance between tool holder and jaws near both travel extremes. Run a shorter member too, since clamp spacing can constrain it differently.
Measure the relationship across the whole part
Check the extreme features from a common datum, then verify the distance between them. Repeat after reloading the same profile family. If the local features pass but the overall span fails, examine the work origin and stock support rather than altering the tool diameter offset.
What to record before production release
Measure the profile from the same reference at the beginning and end of the trial. If a long member shifts at the stop, inspect support height, stock seating and the approved clamping sequence before changing programmed positions.
Related equipment and reading
- Heavy-Duty Aluminum Profile Drilling and Milling Machine
- CNC Axis Travel vs. Maximum Aluminum Profile Length
Send your drawings or samples for review.
Technical reference
Fom Industrie FMC technical sheet. An industry example of documenting working areas, stops, vices and tool configuration independently. It does not specify Jinren capability.