
Aluminum Door Lock Pocket Inspection Before Assembly
Use the real lock body, faceplate and fasteners to verify an aluminum door lock hole milling setup.
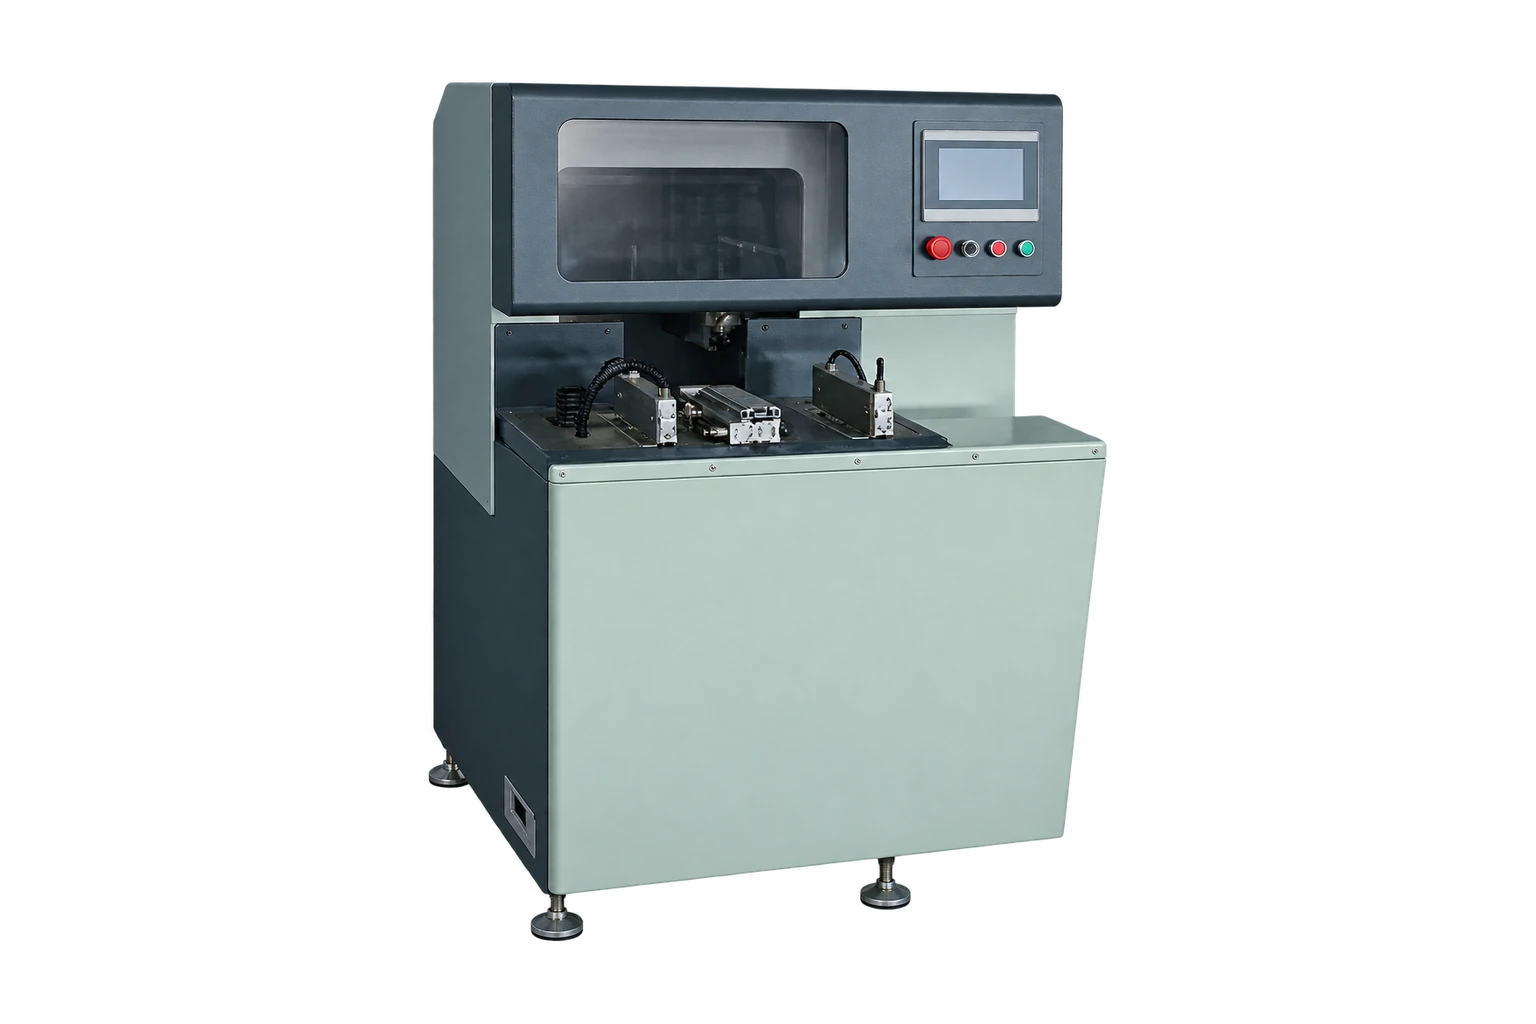
Make the lock supplier drawing the reference
Record the lock model, backset, faceplate dimensions and the required distance from the door datum. Identify the lock body pocket separately from the faceplate recess and fixing holes. Put the approved hardware beside the drawing so a visually similar part cannot silently replace it during the trial.
Measure position before testing insertion
Check pocket location, depth and corner clearance against the drawing. If the lock does not seat, inspect the internal web and the pocket corners for interference. If the body seats but the faceplate stands proud, measure the faceplate recess from the finished profile face. Deburr to the approved process before the fit check.
Verify the assembled function
Install the specified screws and check that they seat without interfering with moving hardware. Verify the cylinder and handle line up when the lock is fully seated. Repeat on a handed pair where required, and record the hardware revision beside the machining program. This catches a mismatch that measuring the empty pocket alone cannot show.
What to record before production release
Keep one approved hardware set at the workstation for the trial. Compare recess depth with the lock removed and flushness with it installed. This separates an incorrect recess from interference caused by the lock body or fastener.
Related equipment and reading
- JR-1400 Single-Head Lock Machining Machine
- CNC Milling Lock Pockets and Concealed Hinges in Aluminum Doors
Send your drawings or samples for review.
Technical reference
Fom Industrie FMC technical sheet. An industry example of documenting working areas, stops, vices and tool configuration independently. It does not specify Jinren capability.