
Choosing CNC Milling Cutters for Aluminum Extrusions
Select an aluminum-profile milling cutter from the slot geometry, required reach and available chip clearance.
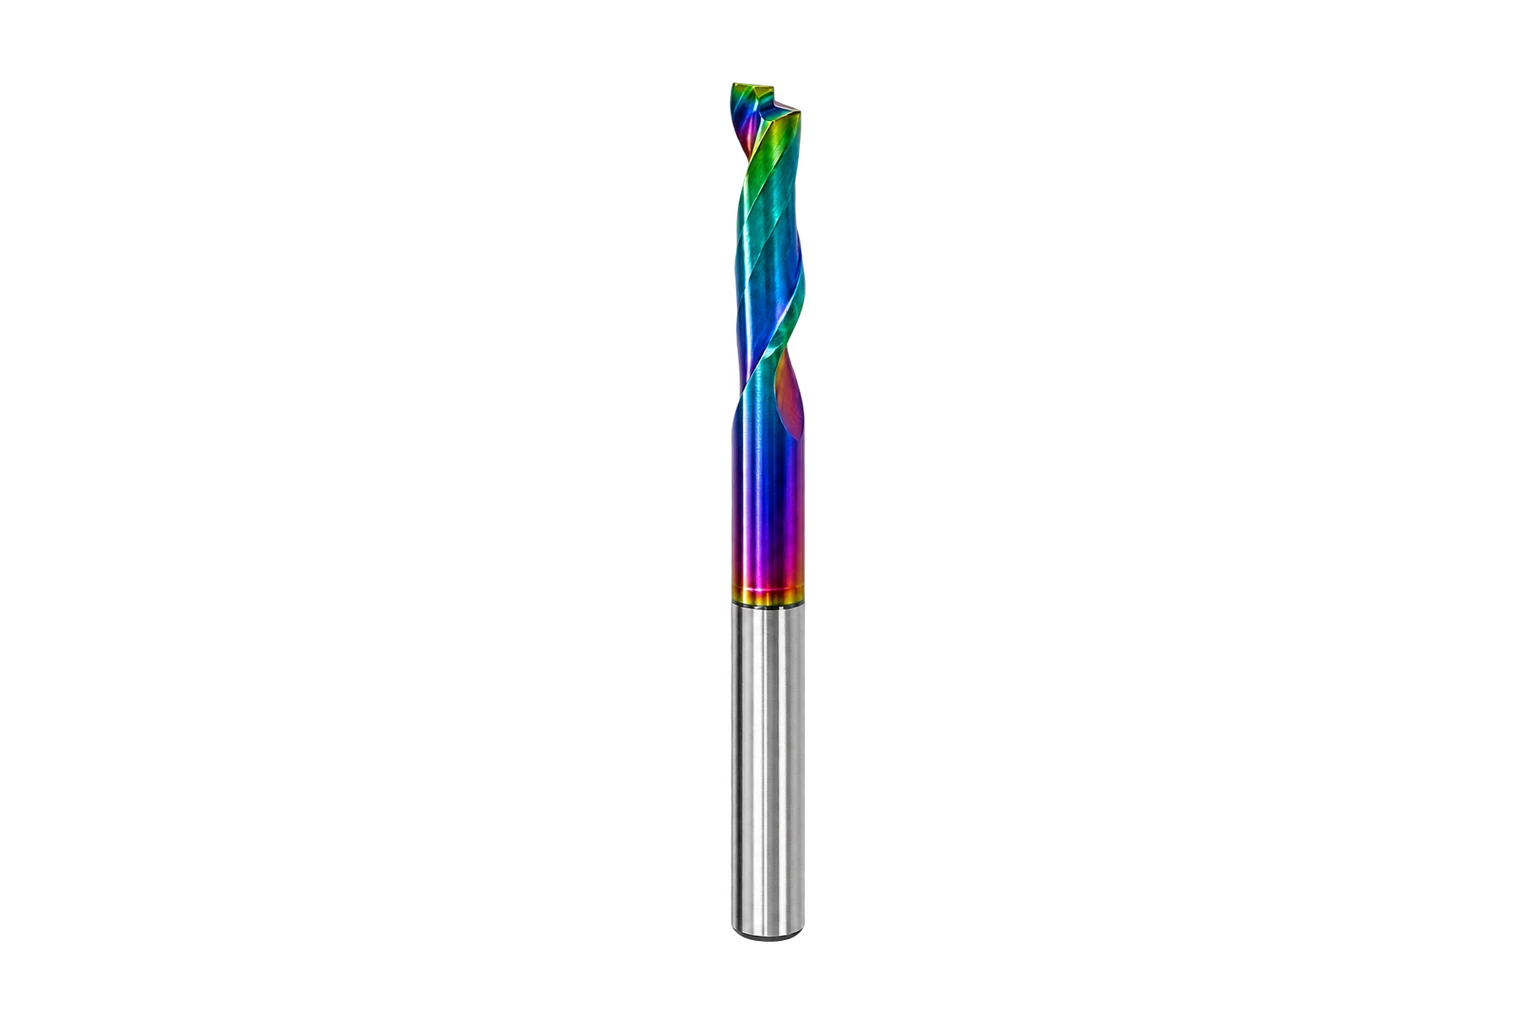
Translate the slot into cutter requirements
Mark slot width, corner radius, depth and entry path. Check cutter diameter and usable flute length, then confirm the shank and holder fit the spindle. Include the jaws and surrounding section in the clearance check. Ask the tool supplier whether the proposed cutter supports the intended entry strategy.
Evaluate chip evacuation on the real pocket
Sandvik Coromant's milling guidance treats chip evacuation as especially relevant in deep cavities. Use the machine and tool makers' recommended settings for your configuration. Inspect whether chips leave the pocket and whether the finish shows smearing or recutting. Check holder condition and tool projection if the surface changes along the slot.
Approve a cutter by repeatable results
Inspect width, depth, burrs and finish over multiple parts, including after a tool change. Record the exact cutter, holder, projection and approved program revision. If tooling is replaced with a different geometry, run a new first-piece check before releasing the batch.
What to record before production release
Include a cross-section of the hardest slot with holder clearance and entry path marked. Keep a photo of the accepted edge finish and record how chips are cleared. If the required finish changes, repeat the trial on the relevant alloy and finish.
Related equipment and reading
Send your drawings or samples for review.
Technical reference
Sandvik Coromant milling application guide. Technical background on cutting edge selection and chip evacuation.