
Custom Fixtures for Aluminum Profile Machining
A fixture locates the extrusion against the drawing datum and holds it without movement or unacceptable surface marks. Stops establish position. Clamps hold the part against the locating surfaces during the cut.
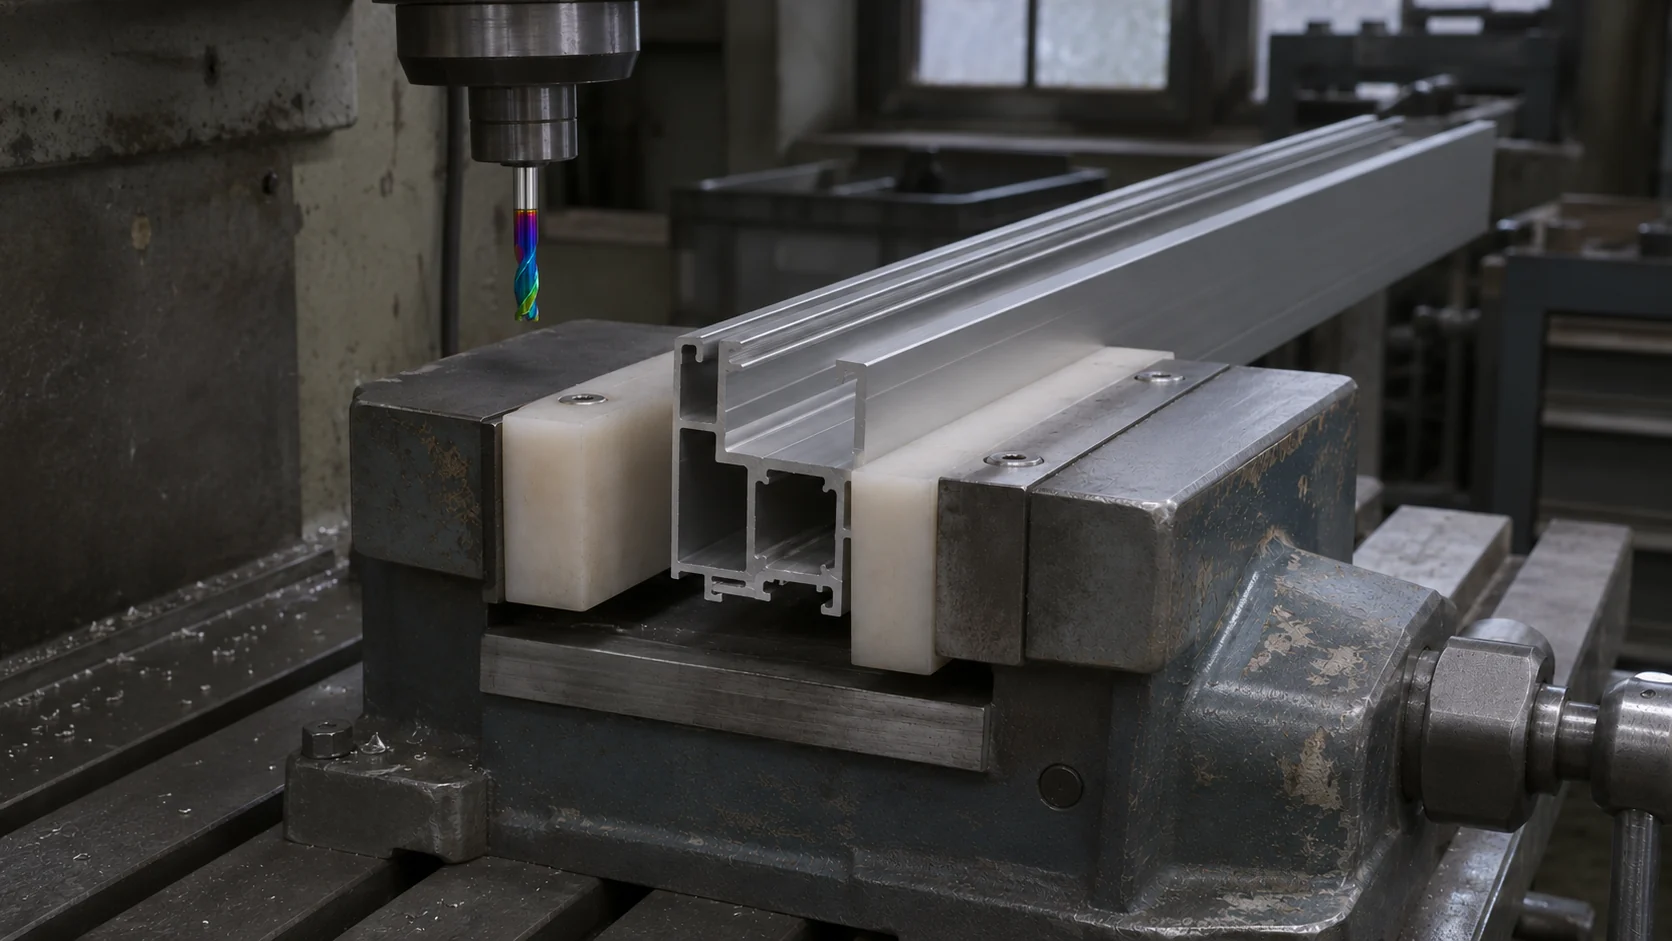
What makes a good profile fixture?
A fixture locates the extrusion against the drawing datum and holds it without movement or unacceptable surface marks. Stops establish position. Clamps hold the part against the locating surfaces during the cut.
How to qualify the fixture
Use the smallest and largest profile sections and a part with a feature beside a clamp. Check that jaws contact supported walls and clear both the tool and holder. Remove and reload parts and inspect the same feature from the same datum. For a flip fixture, check cross-face feature position after the flip. Record approved stop and clamp positions for each profile family.
Related Jinren equipment
- Four-Station CNC Drilling and Milling Machine
- Three-Sided Drilling and Milling Machine for Aluminum Profiles
Discuss your drawings with Jinren.
Technical reference: Fom clamping and head configuration.
What to prepare
Start with the datum scheme on the part drawing. Choose contact faces that are stable and repeatable, and note finished surfaces where even a shallow clamp mark is unacceptable.
What to check during the trial
Check clearance with the cutter and holder at the deepest pocket and nearest clamp. Support thin walls or long overhangs without forcing the profile out of shape.
How to record the decision
Remove and reload the same sample several times, then compare measurements. A repeatability check distinguishes fixture variation from a one-off alignment issue.
When qualifying aluminum profile machining fixtures, measure a datum-to-feature dimension after each reload. Record the clamp positions so a later trial can distinguish setup variation from tool wear.