
Machining Long Aluminum Curtain Wall Profiles
Plan long-profile support and connector feature verification from approved curtain wall fabrication drawings.
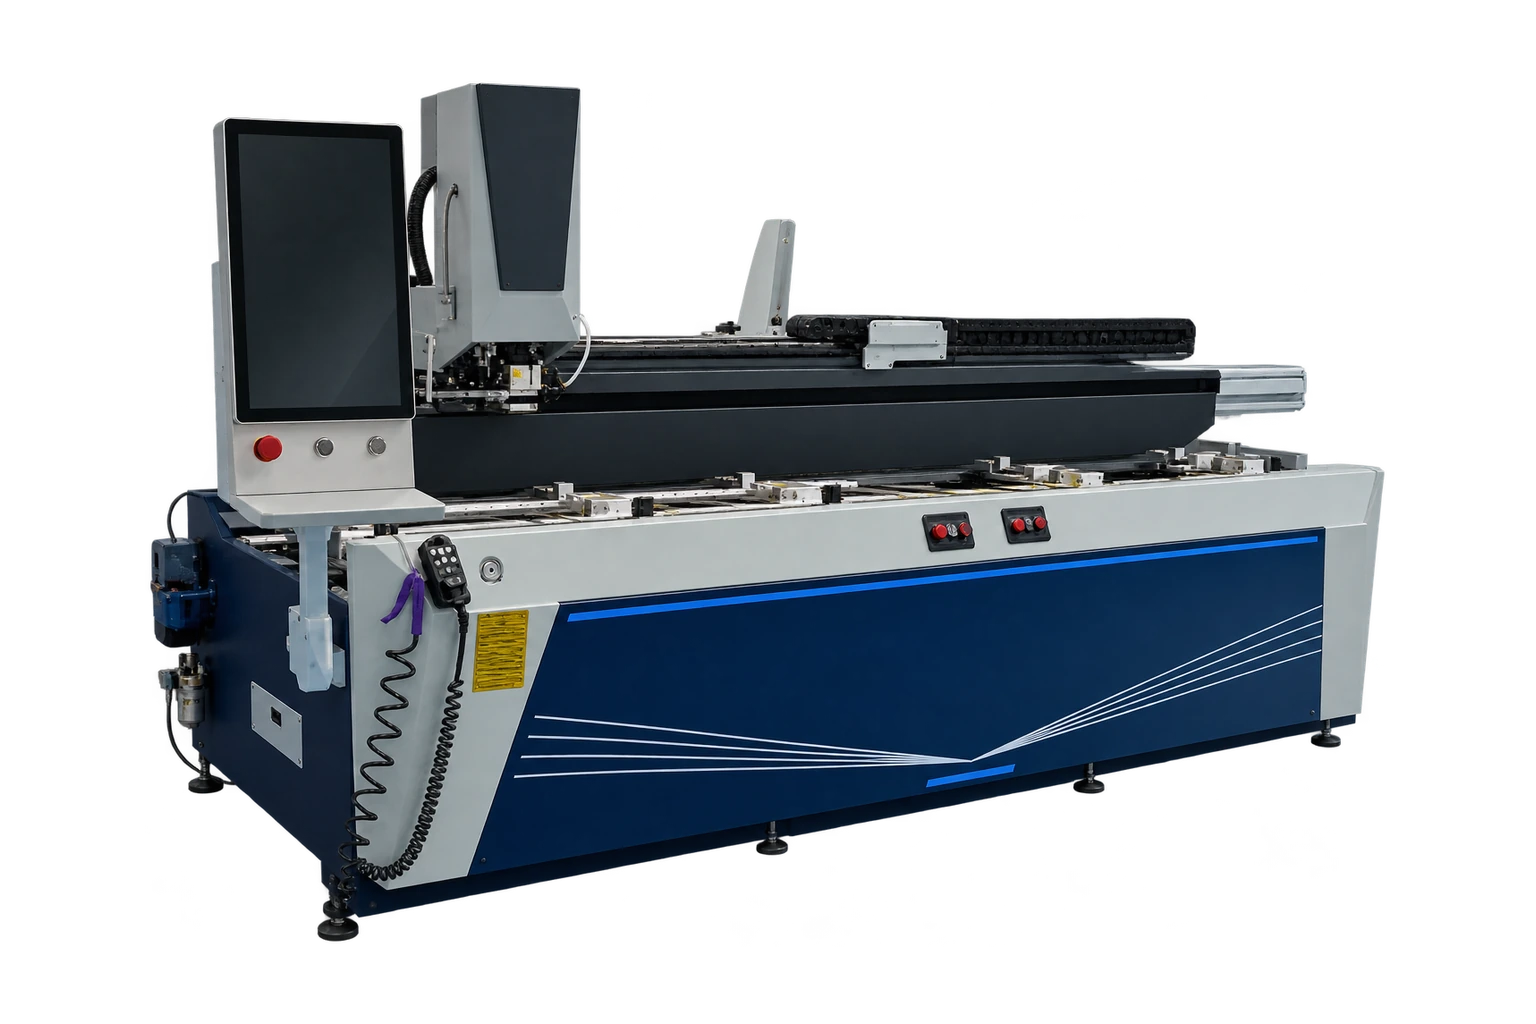
Translate the approved assembly into a machining map
Mark mullion and transom references, profile hand and connector holes. Use the project fabrication package for tolerances and any restrictions on machining structural sections. Separate machining requirements from engineering approval for the finished system.
Verify reach and support on the actual stock
Ask the supplier to demonstrate the outermost holes and slots with the intended holder and clamps installed. Check that the extrusion remains seated at the stop and that supports do not interfere with the tool path. If the part must be repositioned, state how the new setup inherits the original datum.
Measure before and after fitting the connector
Inspect feature positions at both ends and across faces. Then use the specified connector and mating profile to check alignment. Record support positions and the finished measurements. Repeat after reloading to confirm the result can be reproduced in the shop.
What to record before production release
Use separate inspection lines for overall feature spacing and local position at each end. A single tape measurement along the stock cannot establish whether a connector hole is centered on the correct face. Record checks before and after connector fit.
Related equipment and reading
- Heavy-Duty Aluminum Profile Drilling and Milling Machine
- Multi-Face Machining for Long Aluminum Profiles
Send your drawings or samples for review.
Technical reference
Fom Industrie FMC technical sheet. An industry example of documenting working areas, stops, vices and tool configuration independently. It does not specify Jinren capability.
When comparing a CNC milling machine for curtain wall profiles, include the connector feature farthest from the finished-end datum. Inspect its position before and after the connector is fitted.