
Multi-Face Machining for Long Aluminum Profiles
Plan fixtures and datum checks for long profiles with features on more than one face.
Suggested production workflow
Mark the first and last machining points from the finished datum and show the extrusion cross-section at both ends. Review stock support and holder clearance with the approved clamps installed. If the part must be flipped, check the relationship between features on adjacent faces after reloading. Run both the longest member and the shortest member with close clamp spacing.
Equipment to evaluate
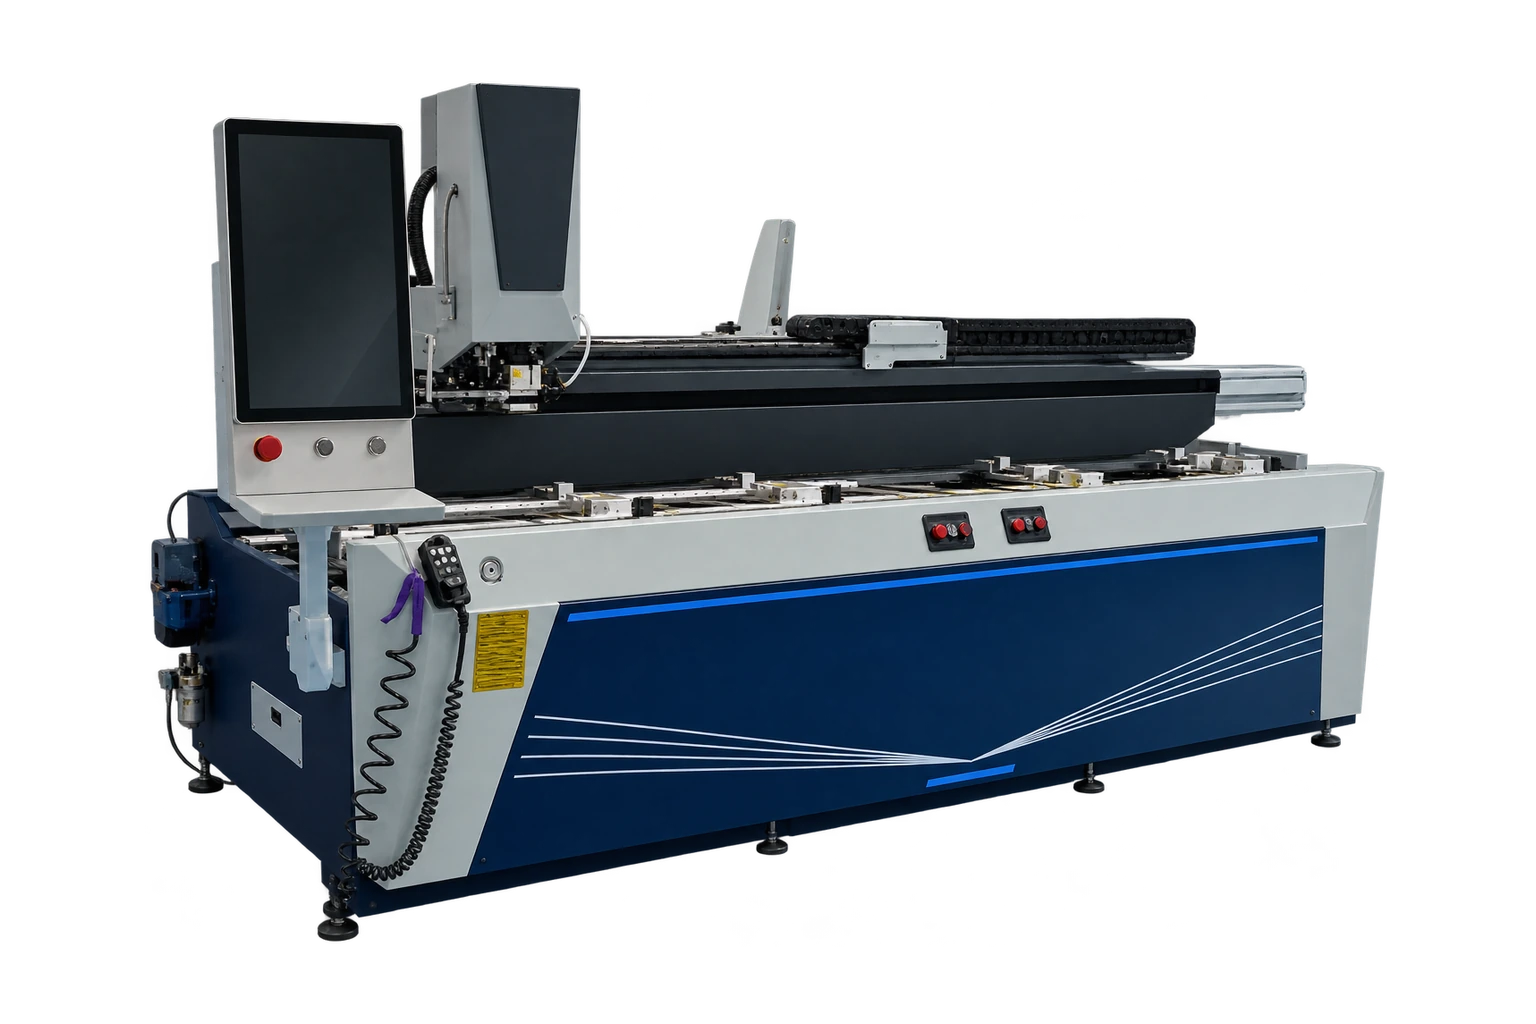
Review the Heavy-Duty Aluminum Profile Drilling and Milling Machine against your drawings and confirm the final setup on a sample run.
What to prepare
Lay out supports and stops using the full stock length, then mark the span of all features. Check whether handling or overhang can twist the section before machining.
What to check during the trial
Place inspection points at both ends and at midspan. Measure indexed faces from the same end reference so end-stop drift and face rotation can be distinguished.
How to record the decision
For the longest sample, compare supported and released measurements if the drawing requires it. Record setup changes and sample acceptance before increasing batch size.